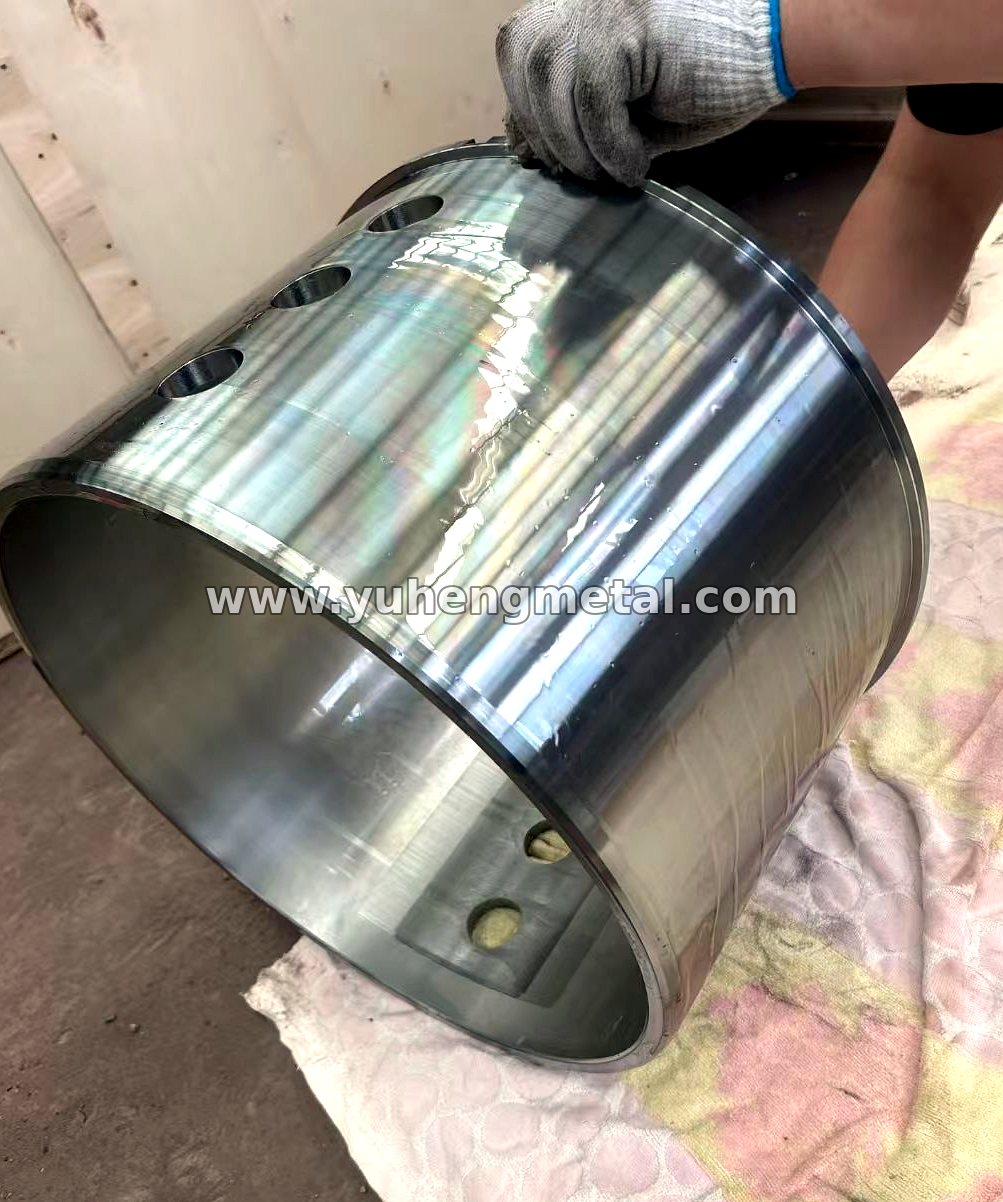
Pick up a Babbitt bearing shell and you can mark the lining with a fingernail. That same lining carries hundreds of tons of kiln, turbine or mill shafts on a film of oil thinner than a human hair. Understanding why that works - and where it stops working - is most of what you need in order to specify, fit and look after these bearings.
The melting point of Babbitt (white metal)
A white metal bearing - Babbitt - is a low-melting-point alloy by design, and its melting point is one of the first things engineers ask about, in steel-mill roll-neck and turbine bearings as much as anywhere. Tin-based Babbitt melts at about 430-470 °F (220-245 °C); lead-based Babbitt melts a little higher, at about 460-480 °F (235-250 °C). By ASTM B23 grade:
| Grade (ASTM B23) | Base | Melting point |
|---|---|---|
| Grade 1 | tin | about 433 °F (223 °C) |
| Grade 2 | tin | about 466 °F (241 °C) |
| Grade 3 | tin | about 464 °F (240 °C) |
| Grade 7 | lead | about 464 °F (240 °C) |
| Grade 8 | lead | about 459 °F (237 °C) |
| Grade 15 | lead | about 479 °F (248 °C) |
Melting point is not the working limit: Babbitt softens long before it melts - Grade 2 falls from roughly 24 HBW at 68 °F (20 °C) to about 12 HBW at 212 °F (100 °C). It is the oil-film temperature, not the melting point, that sets a safe running limit.
What Babbitt metal actually is
Babbitt metal - also called white metal, whitemetal or simply bearing metal - is a low-melting-point bearing alloy named after Isaac Babbitt, who patented the first version in 1839. It is not one material but a family, and two branches of it matter commercially:
- Tin-based Babbitt - tin with antimony and copper, typically around 8% antimony with 4% copper, or the higher-antimony grades. This gives the best conformability and corrosion resistance and remains the standard for turbines, generators, large pumps and other high-speed machinery.
- Lead-based Babbitt - lead with antimony and tin. Cheaper, usable at slightly higher temperatures, lower load capacity, and increasingly avoided where lead content is restricted.
The microstructure is the whole trick. A soft matrix carries hard intermetallic particles - tin-antimony cubes and needle-like copper-tin compounds - distributed evenly through it. The hard particles take the load and resist wear; the soft matrix yields, conforms to the journal and lets grit embed instead of scoring the shaft.
Why the lining is thin, and why thin is the point
Babbitt has low fatigue strength, so it is almost never used as a solid bearing. It is bonded as a thin layer - commonly 1 to 5 mm, and thinner still on high-speed machines - onto a steel, cast-iron or bronze shell back. That combination is what engineers mean by a bearing shell: a strong back carrying a soft, conformable surface.
Thin is not a compromise, it is a requirement. The thinner the lining, the higher the load it can carry before fatigue sets in, and the more easily heat escapes from the bearing surface. A lining that is too thick fails early; one that is the right thickness and properly bonded outlasts the maintenance interval.
How an oil-film bearing carries load
At running speed the journal drags oil into the converging gap between itself and the shell, building a pressure wedge that lifts the shaft clear of the metal. On a healthy machine the two surfaces never touch - the load rides on the film. The lining earns its keep in the moments when that film is not there:
- Start-up and shut-down, when the shaft turns too slowly to build a film
- Stops under load, when oil drains away and the journal rests on the shell
- Overload and misalignment, when the film thins at the edge of the bearing
- Contaminated oil, when grit passes through the film
In every one of those cases the soft lining yields, embeds the particle or wears preferentially - and the expensive shaft survives. That is the bargain a Babbitt bearing makes with its machine.
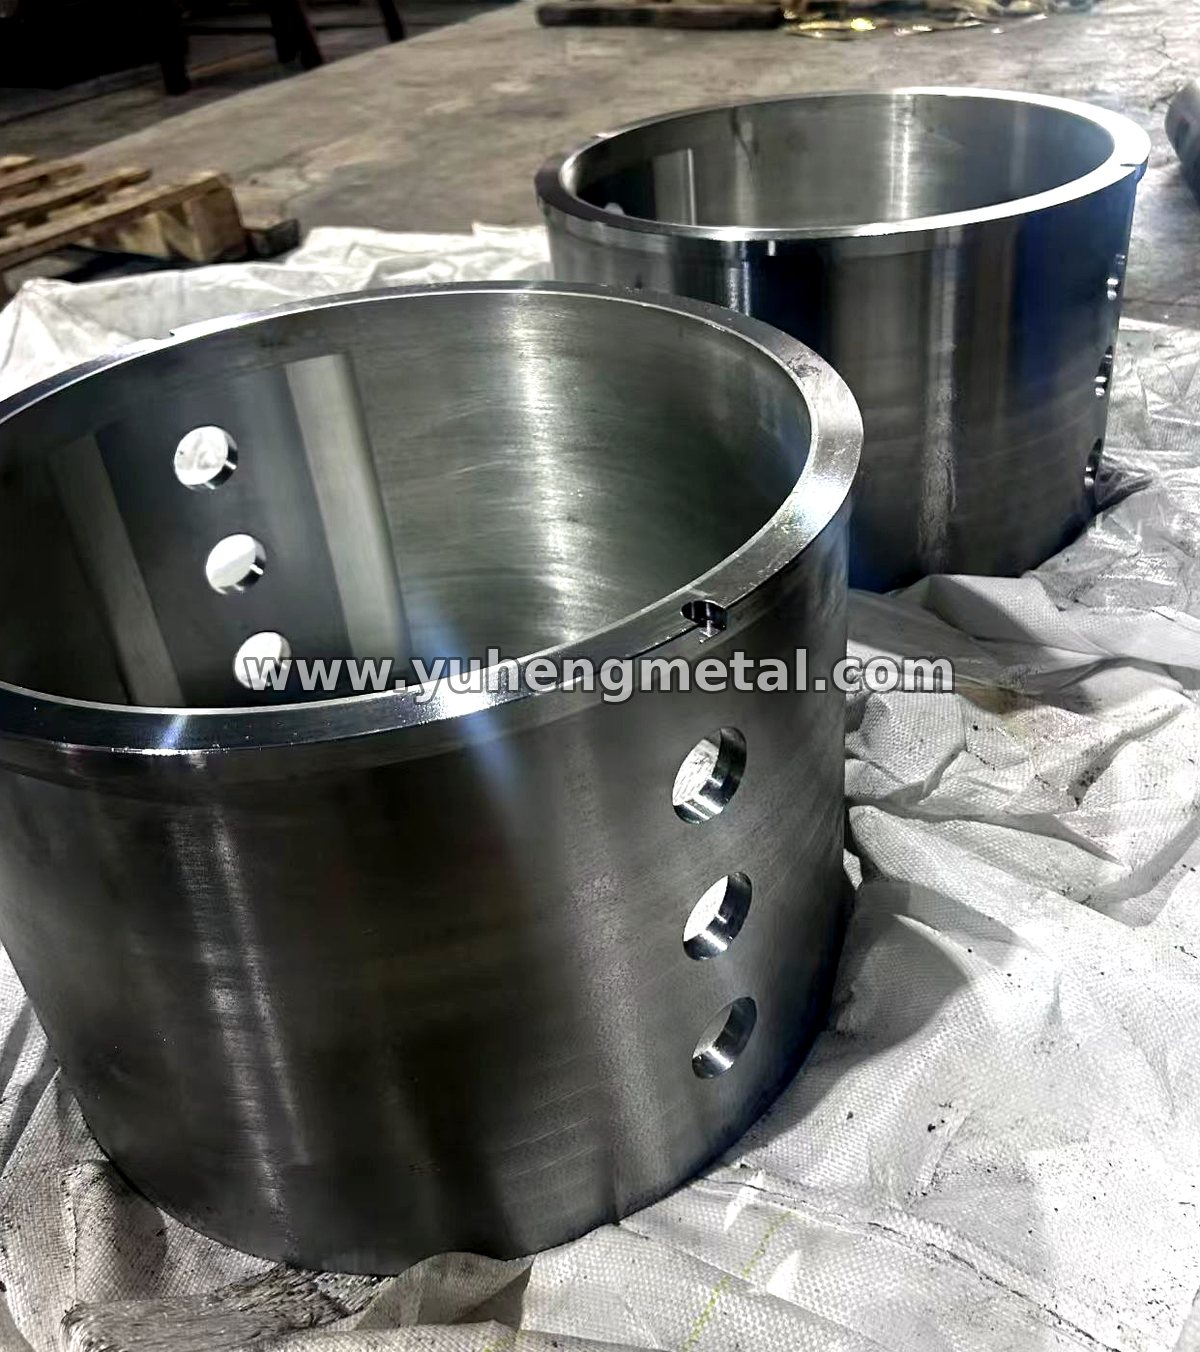
Tin Babbitt vs lead Babbitt
Tin-based and lead-based Babbitt are the two families in commercial use. They differ in base metal, melting point, load capacity and cost, and the choice between them decides how the bearing behaves in service.
| Property | Tin-based Babbitt | Lead-based Babbitt |
|---|---|---|
| Typical composition | Sn with 7-8% Sb, 3-4% Cu | Pb with 10-15% Sb, 1-10% Sn |
| Melting point | about 430-470 °F (220-245 °C) | about 460-480 °F (235-250 °C) |
| Load capacity | high | moderate |
| Temperature capability | about 130 °C for continuous duty, up to about 150 °C (ASTM Grade 2) | similar, with lower load capacity |
| Corrosion resistance | good | poorer; sensitive to water and acidic oil |
| Relative cost | higher (tin content) | lower |
| Typical use | turbines, generators, large pumps, high-speed shafts | general industrial bearings where cost drives the choice |
For kiln, mill, pump and gearbox duties, the choice is usually between a standard tin-based grade and a leaded alternative. Where the machine is a turbine or a high-speed generator, tin-based is the only sensible answer.
Babbitt, bronze or zinc-based: which lining for the duty
Most enquiries that arrive as "Babbitt bearing" turn out to be a choice between four families. The table below is the version we use on the shop floor when a customer sends a drawing and a duty, and it is deliberately qualitative - the numbers that decide a bearing are clearance, oil film and temperature, not a single strength figure.
| Lining | Load capacity | Speed | Conformability / dirt tolerance | Lubrication | Where it belongs |
|---|---|---|---|---|---|
| Tin-based Babbitt (ASTM B23 Grade 2, 3) | High, when the lining stays thin and bonded | Very high | Excellent - embeds grit, tolerates misalignment | Continuous oil film essential | Turbines, generators, high-speed pumps and fans, mill pinions |
| Lead-based Babbitt (Grade 7, 8, 15) | Moderate | High | Excellent | Continuous oil film essential | General industrial shafts where cost drives the choice and no water or acidic oil is present |
| Tin / leaded bronze (copper alloy castings) | High | Moderate to high | Good - less forgiving of dirt than Babbitt | Oil or grease; survives short interruptions better | Crushers, mill pinions, low-speed heavy shafts, bushings with a grease point |
| Zinc-based ZA303 (zinc-based bearings) | High for a solid bearing at moderate speed | Low to moderate | Fair - needs good alignment and a generous clearance | Oil or grease; runs marginal where a Babbitt would wipe | Kiln trunnion pads, liner plates, replacements where speed is low and load is steady |
The short version: if the shaft is fast enough to build a proper oil film, Babbitt is still the best surface in the plant. If the duty is slow, heavy and greased, a solid bronze or zinc-based alloy saves both the relining interval and the cost. Where a machine has been converted from Babbitt to zinc-based, check the clearance - zinc alloys expand more than steel, so the cold clearance has to be wider than the Babbitt figure on the old drawing.
Four questions settle most cases: how fast does the shaft turn, how heavy is the load per unit of projected area, how hot does the housing run, and how good is the lubrication? Answer those and the family picks itself. If two families still fit, send us the drawing and the duty and we will say which one we would cast.
How the shells are made
- Back preparation. The steel or cast-iron back is degreased and cleaned back to bright metal, then tinned, so the lining bonds metallurgically rather than merely sitting on the surface.
- Casting. Static (gravity) casting suits pads and irregular shells; centrifugal casting suits cylindrical bushes and gives a finer grain, a better bond and less porosity.
- Cooling control. Cooling rate decides the size and distribution of the hard particles and the amount of shrinkage porosity, and it is where most of the skill in the process lives.
- Bond testing. The finished lining is checked for debonding - by ultrasonic inspection or hammer testing. A lining that has lifted from its back will fail in service no matter how good it looks.
- Machining. Bore, faces, oil grooves, oil holes, keyways and dowel holes are cut to drawing, with the bore held to the specified running clearance rather than to a nominal size.
- Fitting and despatch. Clearance and contact pattern are checked before the shell is packed, because a shell that fits cold rarely behaves badly when hot.
How they fail - and what the failure tells you
- Wiping. The lining smears when temperature rises or oil supply is interrupted. Look at oil flow, viscosity, clearance and load, not at the bearing.
- Fatigue. Cracking and spalling of the lining under cyclic load, usually made worse by edge loading from misalignment or by a lining that is thicker than the duty needs.
- Debonding. The lining lifts away from the back after poor tinning, contamination or repeated thermal cycling. The cure is stripping and re-lining, not shimming.
- Contamination. Embedded grit in the surface means the oil is carrying dirt; the answer is filtration, and making the oil circuit prove it.
- Corrosion. Water ingress or acidic oil attacks lead-based grades first. Check the oil and the cooler, and consider a tin-based lining.
Replacing a worn shell
Most of the shells and bushes we make are replacements rather than original equipment parts. Send the worn shell, a drawing, or a photo with the main dimensions and we measure, reverse-engineer, cast, bond and machine to fit. Where the original documentation is missing, the numbers that matter are the housing bore, the journal diameter, the lining thickness the housing allows, the position of the oil ways, and the retention arrangement - keyway, dowel or nip.
Before the new shell goes into service, check the contact pattern, set the babbitt bearing clearance, confirm that oil reaches the load zone through the grooves, and watch the temperature rise during the first hours of running. A bearing that runs cool after a re-fit usually keeps running cool.
Questions we get asked
What is the difference between Babbitt and bronze?
Babbitt is a soft, low-melting tin or lead based alloy used as a thin lining bonded to a steel or cast-iron back. Bronze is a solid copper-based bearing alloy. Babbitt conforms to the journal and embeds dirt better; bronze carries more load and tolerates higher temperature.
What is the melting point of a white metal bearing (Babbitt)?
Tin-based Babbitt melts at about 430-470 °F (220-245 °C), and lead-based Babbitt a little higher at about 460-480 °F (235-250 °C). By ASTM B23 grade: Grade 1 about 433 °F (223 °C), Grade 2 about 466 °F (241 °C), Grade 3 about 464 °F (240 °C); lead-based Grade 7 about 464 °F (240 °C), Grade 8 about 459 °F (237 °C), Grade 15 about 479 °F (248 °C). Melting point is not the working limit: Babbitt softens long before it melts - Grade 2 falls from roughly 24 HBW at 68 °F (20 °C) to about 12 HBW at 212 °F (100 °C). It is the oil-film temperature, not the melting point, that sets a safe running limit.
What is the difference between tin Babbitt and lead Babbitt?
Tin-based Babbitt gives the best conformability and corrosion resistance and carries the highest loads; it is the standard for turbines, generators, pumps and other high-speed shafts. Lead-based Babbitt is cheaper and tolerates slightly higher temperature, but it carries less load and resists water and acidic oil poorly. Where lead content is restricted, tin-based is the safe choice.
Can a Babbitt bearing run without oil?
No. Babbitt depends on an oil film. Dry running destroys the lining within minutes, and even a short stop under load with no oil feed marks the surface. Restoring oil flow and cooling is always more urgent than the bearing itself.
How thick should the Babbitt lining be?
For most industrial shells and pads, 1 to 5 mm of lining on a sound backing. Thinner linings carry higher loads without fatigue but demand better bonding and a straighter housing, while thick linings are more forgiving to cast but fail earlier.
Can you make a replacement shell from our worn part?
Yes. Send the worn shell, a drawing or a photo with the main dimensions - housing bore, journal diameter, lining thickness, oil-way positions and the retention arrangement. We reverse-engineer, cast, bond and machine to fit.
How many types of Babbitt bearings are there?
Two families, split by the base metal. Tin-based Babbitt (ASTM B23 Grade 1, 2 and 3) is tin with about 7-8% antimony and 3-4% copper: the higher load capacity, used for turbines, generators and high-speed shafts. Lead-based Babbitt (Grade 7, 8 and 15) is lead with 10-15% antimony and 1-10% tin: cheaper, for general industrial bearings where water and acidic oil are absent. Within a family the grades differ mainly in hardness and melting point - Grade 2 melts near 241 °C, Grade 15 near 248 °C. The form is a separate question: solid cast bushes, steel shells lined with Babbitt and re-lined worn shells all use the same grades.
What is Babbitt bearing metal made of?
Babbitt is a low-melting white metal based on tin or lead, hardened with antimony and a little copper. Tin-based: roughly 7-8% antimony, 3-4% copper, balance tin, melting about 220-245 °C. Lead-based: roughly 10-15% antimony, 1-10% tin, balance lead, melting about 235-250 °C. The soft matrix embeds grit instead of scoring the journal, which is why the lining stays thin and why a worn shell is re-poured instead of replaced.
What are the advantages and disadvantages of a Babbitt bearing lining?
Advantages: excellent conformability, so it tolerates slight misalignment; it embeds dirt and grit instead of scoring the journal; low friction on an oil film; and it is re-pourable, so a worn shell is relined rather than scrapped. Disadvantages: low fatigue strength, so the lining must stay thin and well bonded; a low melting point, so it cannot run hot and loses hardness as temperature rises; and it is useless without a continuous oil film.
Related products
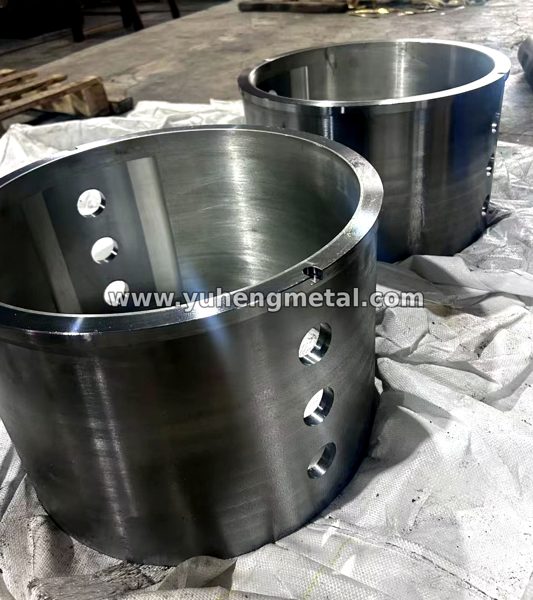 Babbitt & oil-film
Babbitt Bearing Shells & Oil-Film Bearings
Babbitt (white metal) bearing shells and oil-film bearings for heavy-duty rotating equipment - cast, bonded and machined to drawing, in tin-based and lead-based alloys.
Babbitt lining thickness →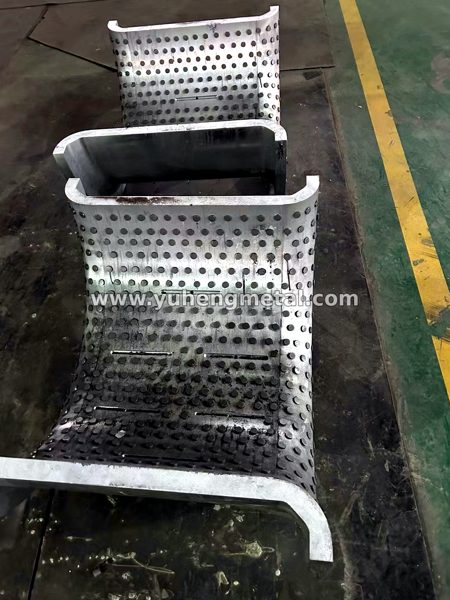 Heavy industry
Rotary Kiln Trunnion & Support Roller Bearings
Wear-resistant trunnion bearings, support-roller bearing pads and hollow-shaft bearings for rotary kilns, dryers and grinding mills.
Trunnion sizes and lead time →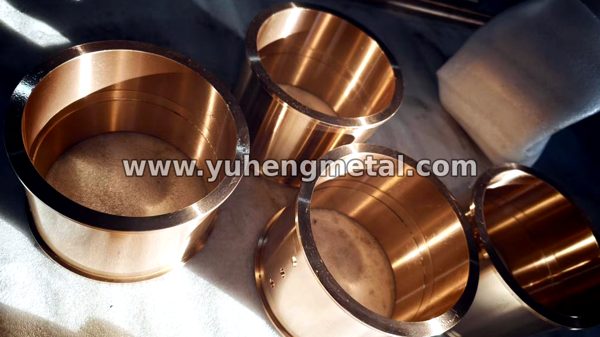 Tin / aluminum bronze
Copper Alloy Castings & Bronze Bushings
Centrifugal and sand-cast copper alloy parts - tin bronze, aluminum bronze and brass bushings, copper sleeves and retaining rings machined to spec.
Bronze grades and processes →Need Babbitt bearing shells?
We cast and machine them to your drawing, or from a worn shell or a site measurement - tin-based and lead-based grades, up to 1,500 mm.